
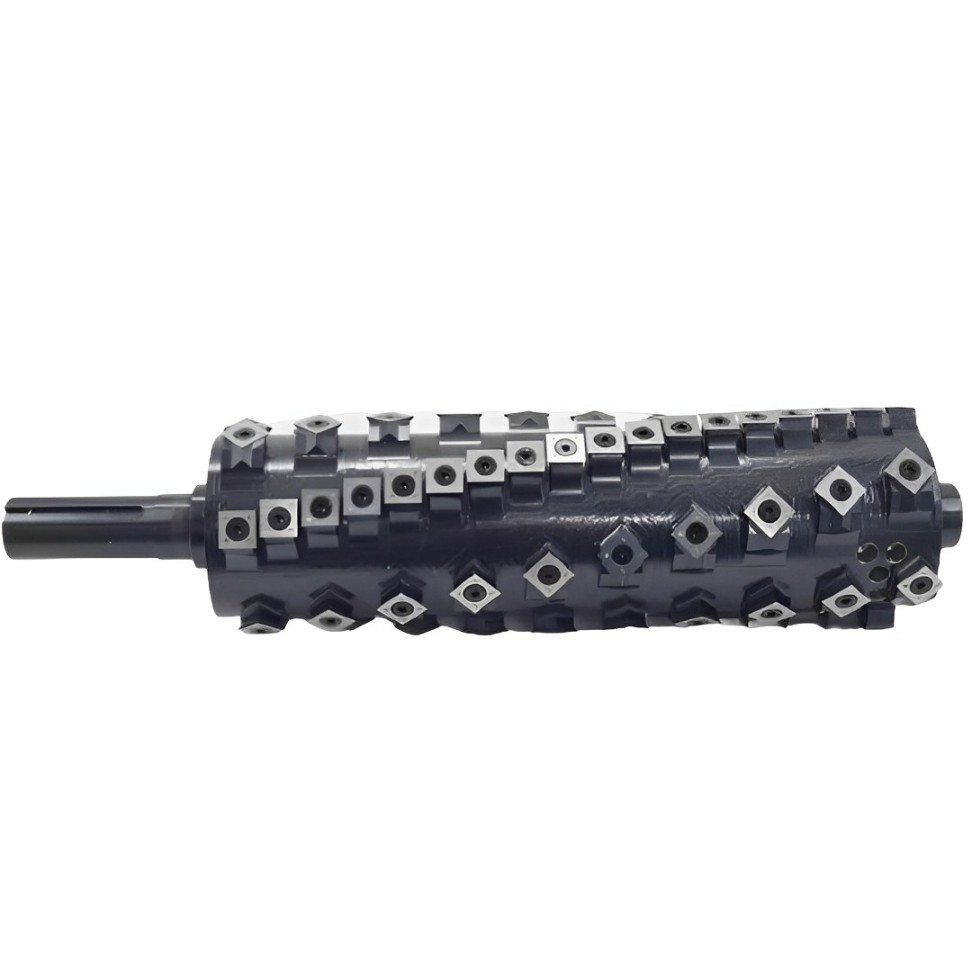
V modernom spracovaní dreva, Spiral Cutter Heads have revolutionized planing and jointing operations by replacing traditional straight-knife designs with indexable carbide inserts arranged in a helical pattern. Tieto inovatívne nástroje poskytujú hladšie povrchy, tichšia prevádzka, a výrazne skrátil čas nastavenia. Avšak, even the most advanced Spiral Cutter Heads can experience performance issues when improperly maintained or operated. Pochopenie ich primárnych funkcií, rozpoznanie spoločných problémov s praktickými riešeniami, and following essential safety practices ensures you maximize the exceptional benefits these cutting systems offer.
Primary Functions of Spiral Cutter Heads in Woodworking
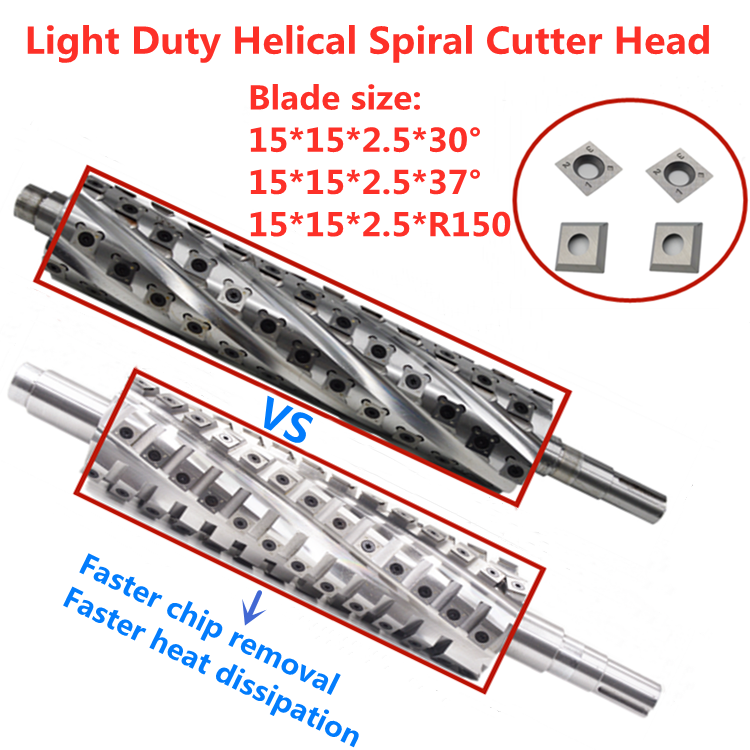
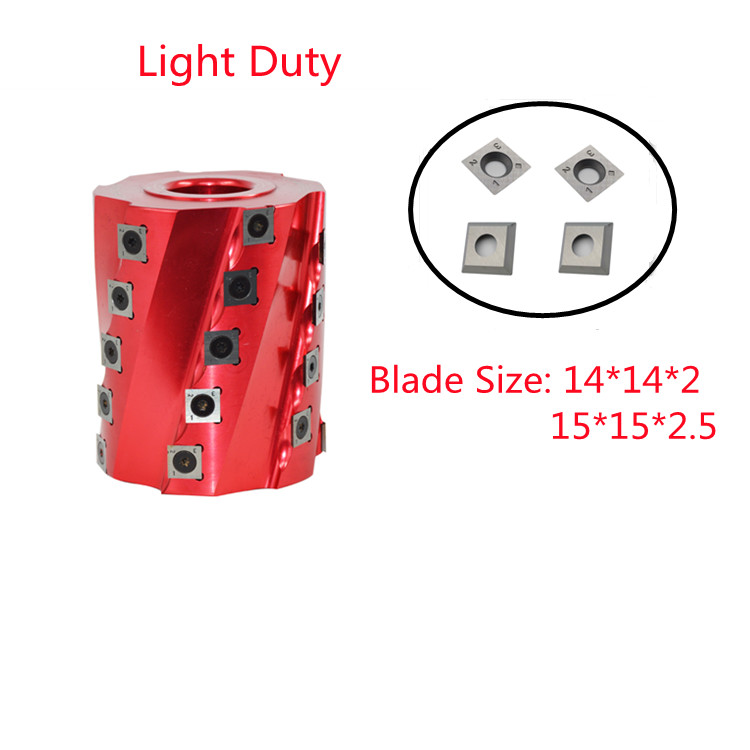
Spiral Cutter Heads serve as the cutting element in planers, škárovačky, a štvorstranné formovače, kde premieňajú hrubé rezivo na rozmerovo presné, hladko hotové dosky. Unlike traditional straight knives that contact the entire workpiece width simultaneously, Spiral Cutter Heads feature multiple small carbide inserts arranged in a helical pattern around the cutterhead body. This geometry creates a shearing cut that reduces tear-out on figured woods, minimizes noise levels, and produces superior surface finishes often requiring no sanding.
Bežné aplikácie zahŕňajú čelné hobľovanie tvrdého a mäkkého dreva, spájanie okrajov na prípravu lepenia, and high-volume dimensioning in production workshops. For cabinet shops, flooring manufacturers, a mlynárske operácie, Spiral Cutter Heads deliver consistent results while eliminating the frustrating process of setting and balancing traditional knives.


Päť bežných problémov a praktických riešení
Problém 1: Uneven or Wavy Surface Finish
Jeden z najviac frustrujúcich problémov s Spiral Cutter Heads is producing boards with washboard patterns, ridges, or inconsistent flatness. This typically indicates feed rate problems, insert damage, or improper cutterhead alignment relative to the bed or table.
Riešenie: Po prvé, verify your feed speed—running too slowly allows each insert to take successive overlapping cuts that create ripples. Increase feed rate within your machine’s recommended range. Po druhé, inspect all carbide inserts for chips or cracks; even one damaged insert leaves a visible ridge. Rotate or replace affected inserts following manufacturer guidelines for Spiral Cutter Heads. Po tretie, check that the cutterhead is parallel to the machine table. Use a dial indicator to measure across the cutterhead length and adjust bearing mounts or gibs as needed. Konečne, ensure infeed and outfeed rollers apply consistent pressure—uneven roller pressure causes board rocking that transfers to the cut surface.
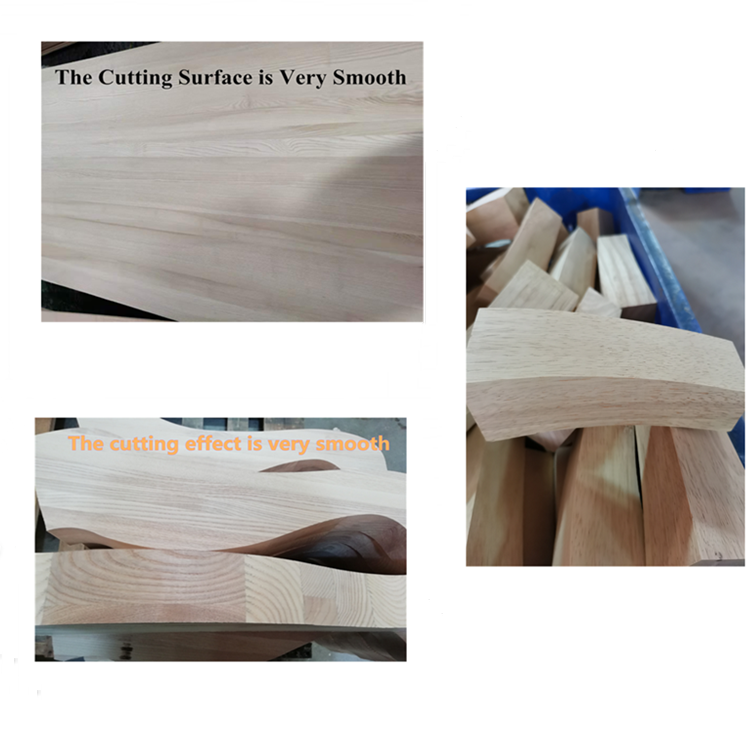
Problém 2: Excessive Insert Breakage or Chipping
Kedy Spiral Cutter Heads suffer frequent insert breakage, vinníkom je zvyčajne náraz cudzieho predmetu, nesprávna technika podávania, alebo použitie nesprávnej triedy doštičky pre spracovávaný materiál. Broken inserts damage workpieces and compromise safety.
Riešenie: Pred hobľovaním vykonajte dôslednú kontrolu reziva – odstráňte všetky klince, svorky, a vložený štrk. Na regenerované alebo stavebné rezivo, consider using a metal detector. Po druhé, vyhýbajte sa kŕmeniu materiálu s voľnými uzlami alebo inklúziami kôry; tieto dopady Spiral Cutter Heads s rázovými zaťaženiami, ktoré lámu karbid. Po tretie, overte, či používate správnu triedu doštičky pre vašu aplikáciu. Standard inserts work well for clean hardwoods and softwoods, ale spracovanie abrazívnych materiálov, ako sú MDF alebo drevotrieskové dosky, si vyžaduje špeciálne potiahnuté vložky alebo vložky s vysokým opotrebením. Konečne, never force material into the cutterhead against the feed direction; always feed with the grain and at consistent speeds.

Premium Craftsmanship: The DH Brand Advantage
For woodworkers seeking exceptional quality and precision, DH brand Spiral Cutter Heads represent a superior choice. Unlike mass-produced alternatives, DH cutterheads are manufactured on advanced five-axis CNC machines, enabling complex geometries and tolerances that standard machining cannot achieve. This precision manufacturing process ensures each cutterhead is perfectly balanced and dimensionally accurate, directly translating to smoother operation and longer bearing life.
Among DH’s extensive product line, the 15×15×2.5×30°-R150 insert has earned particularly widespread customer acclaim. This popular insert size and geometry delivers an ideal balance of cutting efficiency, surface finish quality, and durability across a broad range of woodworking applications. The positive feedback from professionals confirms that DH’s commitment to precision manufacturing and thoughtful insert design genuinely improves daily planing operations.
Problém 3: Burn Marks on Workpiece Surface
Popáleniny na hobľovaných doskách naznačujú nadmerné trecie teplo generované Spiral Cutter Heads. Tento problém zvyčajne pramení z tupých vložiek, nedostatočná rýchlosť posuvu, alebo nahromadenie živice na rezných hranách.
Riešenie: Otočte doštičky, aby ste odhalili čerstvé rezné hrany –Spiral Cutter Heads sú navrhnuté pre ľahké indexovanie, and operators should rotate inserts after every few hours of heavy use. Po druhé, increase feed rate; v rozpore s intuíciou, rýchlejšie podávanie znižuje horenie, pretože každá doštička odoberá hrubšiu triesku, ktorá odvádza teplo preč z reznej zóny. Po tretie, dôkladne vyčistite rezaciu hlavu; pitch and resin accumulated on inserts and between flutes insulates heat and creates friction. Používajte netoxické odstraňovače živice bezpečné pre karbid. Pre živicové drevá ako borovica alebo čerešňa, medzi prechodmi naneste na reznú hlavu špeciálne mazivá alebo vosky. Konečne, reduce depth of cut if burning persists—taking multiple lighter passes generates less friction than one heavy cut.
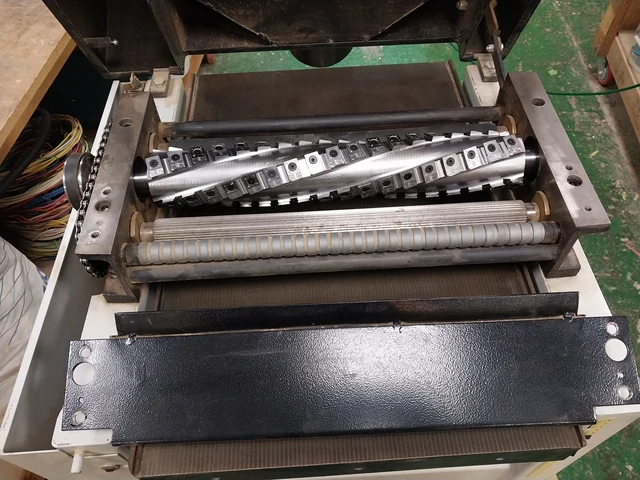
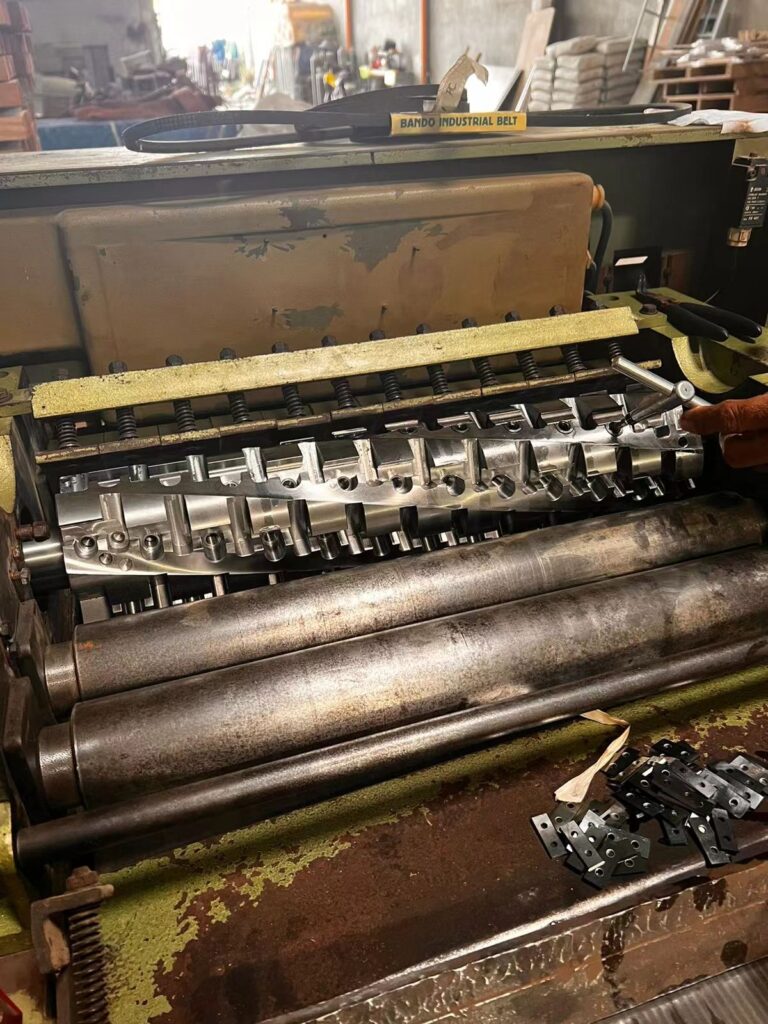
Problém 4: Excessive Noise or Vibration
Zatiaľ čo Spiral Cutter Heads are inherently quieter than straight-knife designs, unusual noise or vibration indicates problems including loose inserts, unbalanced cutterhead components, or bearing failure.
Riešenie: Okamžite zastavte stroj, keď sa objaví abnormálny hluk. Check that all insert screws are tightened to manufacturer specifications—loose inserts produce rattling sounds and dangerous flying debris. Po druhé, inspect Spiral Cutter Heads for missing inserts or broken carbide pieces that unbalance the rotating assembly. Po tretie, remove any debris or resin buildup that could affect balance. Po štvrté, check cutterhead bearings for play or roughness; worn bearings allow cutterhead wobble that creates vibration. Replace bearings as a pair if any issues are detected. Konečne, have the cutterhead professionally balanced if vibration persists after addressing inserts and bearings.
Problém 5: Poor Dust Collection Performance
Kedy Spiral Cutter Heads generate excessive chips that fail to evacuate properly, the resulting chip packing causes insert damage, slabé prevedenie, and fire hazards. This problem typically occurs with machines having inadequate dust hoods or restricted ducting.
Riešenie: Verify that your dust collector provides adequate airflow (measured in CFM) for your machine’s cutterhead size and feed rate. Spiral Cutter Heads produce chips differently than straight knives—smaller, more uniform chips that require efficient air velocity for transport. Clean all dust hoods and duct elbows of accumulated debris. Ensure the dust hood is positioned correctly; many machines have adjustable hoods that must sit within millimeters of the cutterhead for optimal chip capture. For deep cuts, consider reducing depth of pass to decrease chip volume. Never allow chips to recirculate in the cutting zone, as this causes insert impact damage.
Essential Safety Recommendations for Spiral Cutter Heads
Práca s Spiral Cutter Heads requires respect for their rotating mass and the high speeds at which they operate. Pred vykonaním akejkoľvek kontroly vždy odpojte napájanie a nechajte reznú hlavu úplne zastaviť, čistenie, alebo otočenie vložky. Nikdy nesiahajte do stroja, keď sa rezná hlava otáča –Spiral Cutter Heads can cause severe lacerations despite their shearing cut action. Wear hearing protection; even quieter designs generate noise levels requiring rated earplugs or muffs.
Pri hobľovaní krátkych alebo úzkych materiálov používajte tlačné bloky alebo elektrické podávače; ruky sa nikdy nesmú priblížiť k oblasti rezacej hlavy. Inspect Spiral Cutter Heads before each use for loose inserts, damaged pockets, or unusual wear patterns. Ensure all guards and anti-kickback devices are in place and functioning properly. When rotating inserts, wear cut-resistant gloves to protect against sharp carbide edges. Konečne, receive thorough training on your specific machine’s lockout/tagout procedures before performing any maintenance on Spiral Cutter Heads.


Záver
Spiral Cutter Heads have transformed woodworking planing and jointing operations through superior surface finishes and reduced maintenance demands. Premium options like DH brand cutterheads, manufactured on precision five-axis machinery with popular insert configurations such as the 15×15×2.5×30°-R150, demonstrate how quality engineering directly improves cutting performance and customer satisfaction. By understanding primary functions and recognizing the common issues outlined above—uneven finish, zlomenie vložky, stopy po popáleninách, nadmerný hluk, and poor dust collection—operators can implement practical solutions that restore performance and extend component life.
Pravidelné otáčanie vložky, správne rýchlosti posuvu, dôkladné čistenie, a dodržiavanie bezpečnostných postupov to zaisťuje Spiral Cutter Heads poskytujú výnimočné výsledky, na ktoré sú navrhnuté. Pri správnej starostlivosti a prevádzke, these innovative cutterheads turn challenging planing operations into efficient, konzistentné výrobné procesy.
Cutter Head Woodworking Cutter Head Helical Shaper Spiral Jointer